Skip to content

Capabilities

Custom plastic, rubber and silicone components, contract manufactured

We manufacture to customer drawings using four moulding techniques. For each component we design and build the mould in our own workshop, select the material and define the process best suited to the quantities and conditions of use.

Plastic injection moulding

Polymer granules are melted and injected into a custom-designed metal mould. The process produces precise, repeatable components in series, including complex geometries and thin walls.

Process stages

  1. Material preparation The granules are fed into the hopper; hygroscopic polymers such as PA 6, PA 66 and PC are dried first, to prevent surface and structural defects.
  2. Melting and injection The material melts in the plasticising barrel at between 120 °C and 360 °C and is injected into the closed mould. For overmoulding onto metal inserts, the inserts are placed in the mould before it closes.
  3. Cooling and solidification Cooling channels built into the mould ensure dimensional stability.
  4. Ejection from the mould Ejector pins remove the part and the sprue is removed.

Co-design

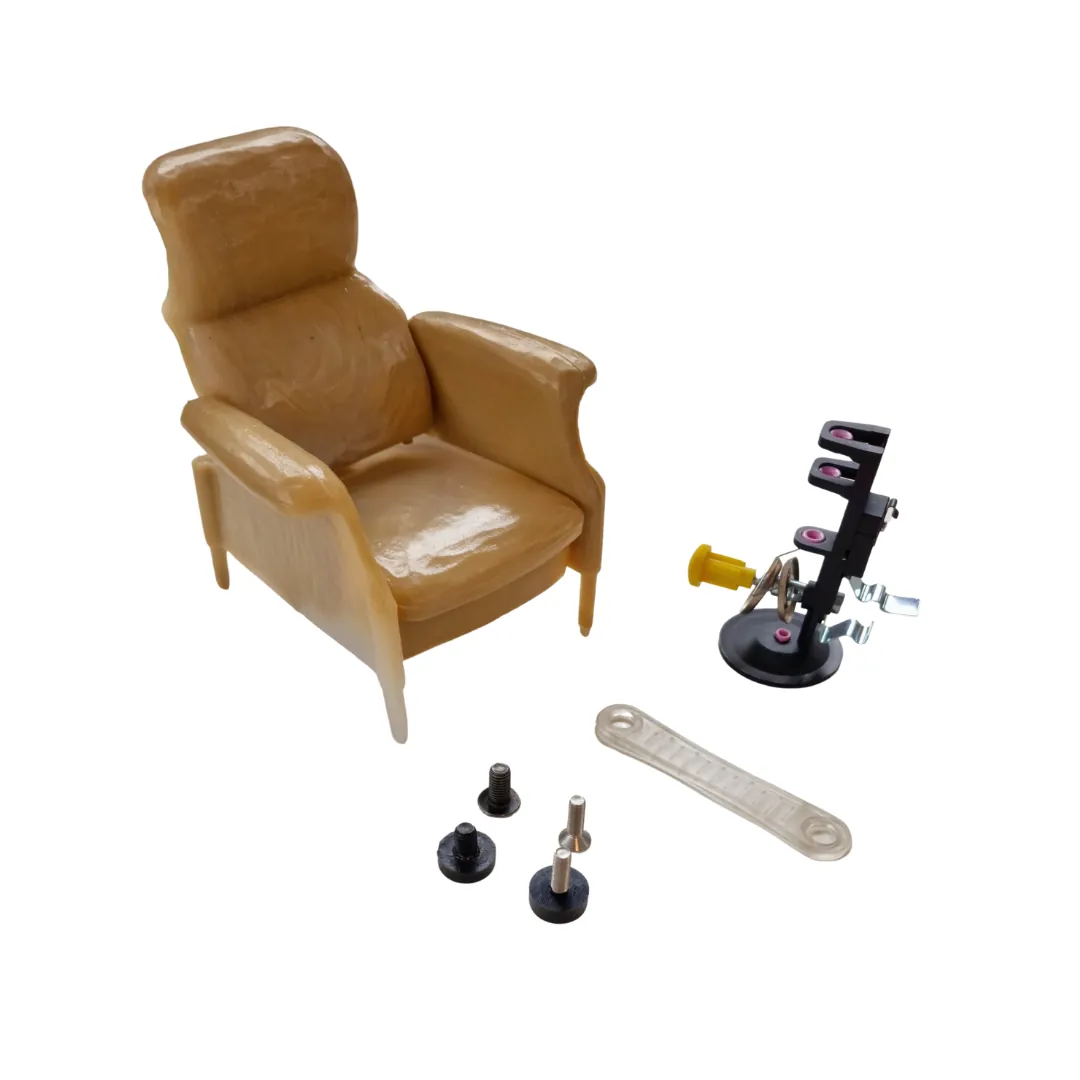
CAD modelling and 3D prototyping make it possible to optimise geometry and material at the design stage.

When it is the right choice

For series production, when volumes justify the cost of the mould. For prototypes and small batches 3D printing is more suitable; for rubber articles or simple geometries, compression moulding.
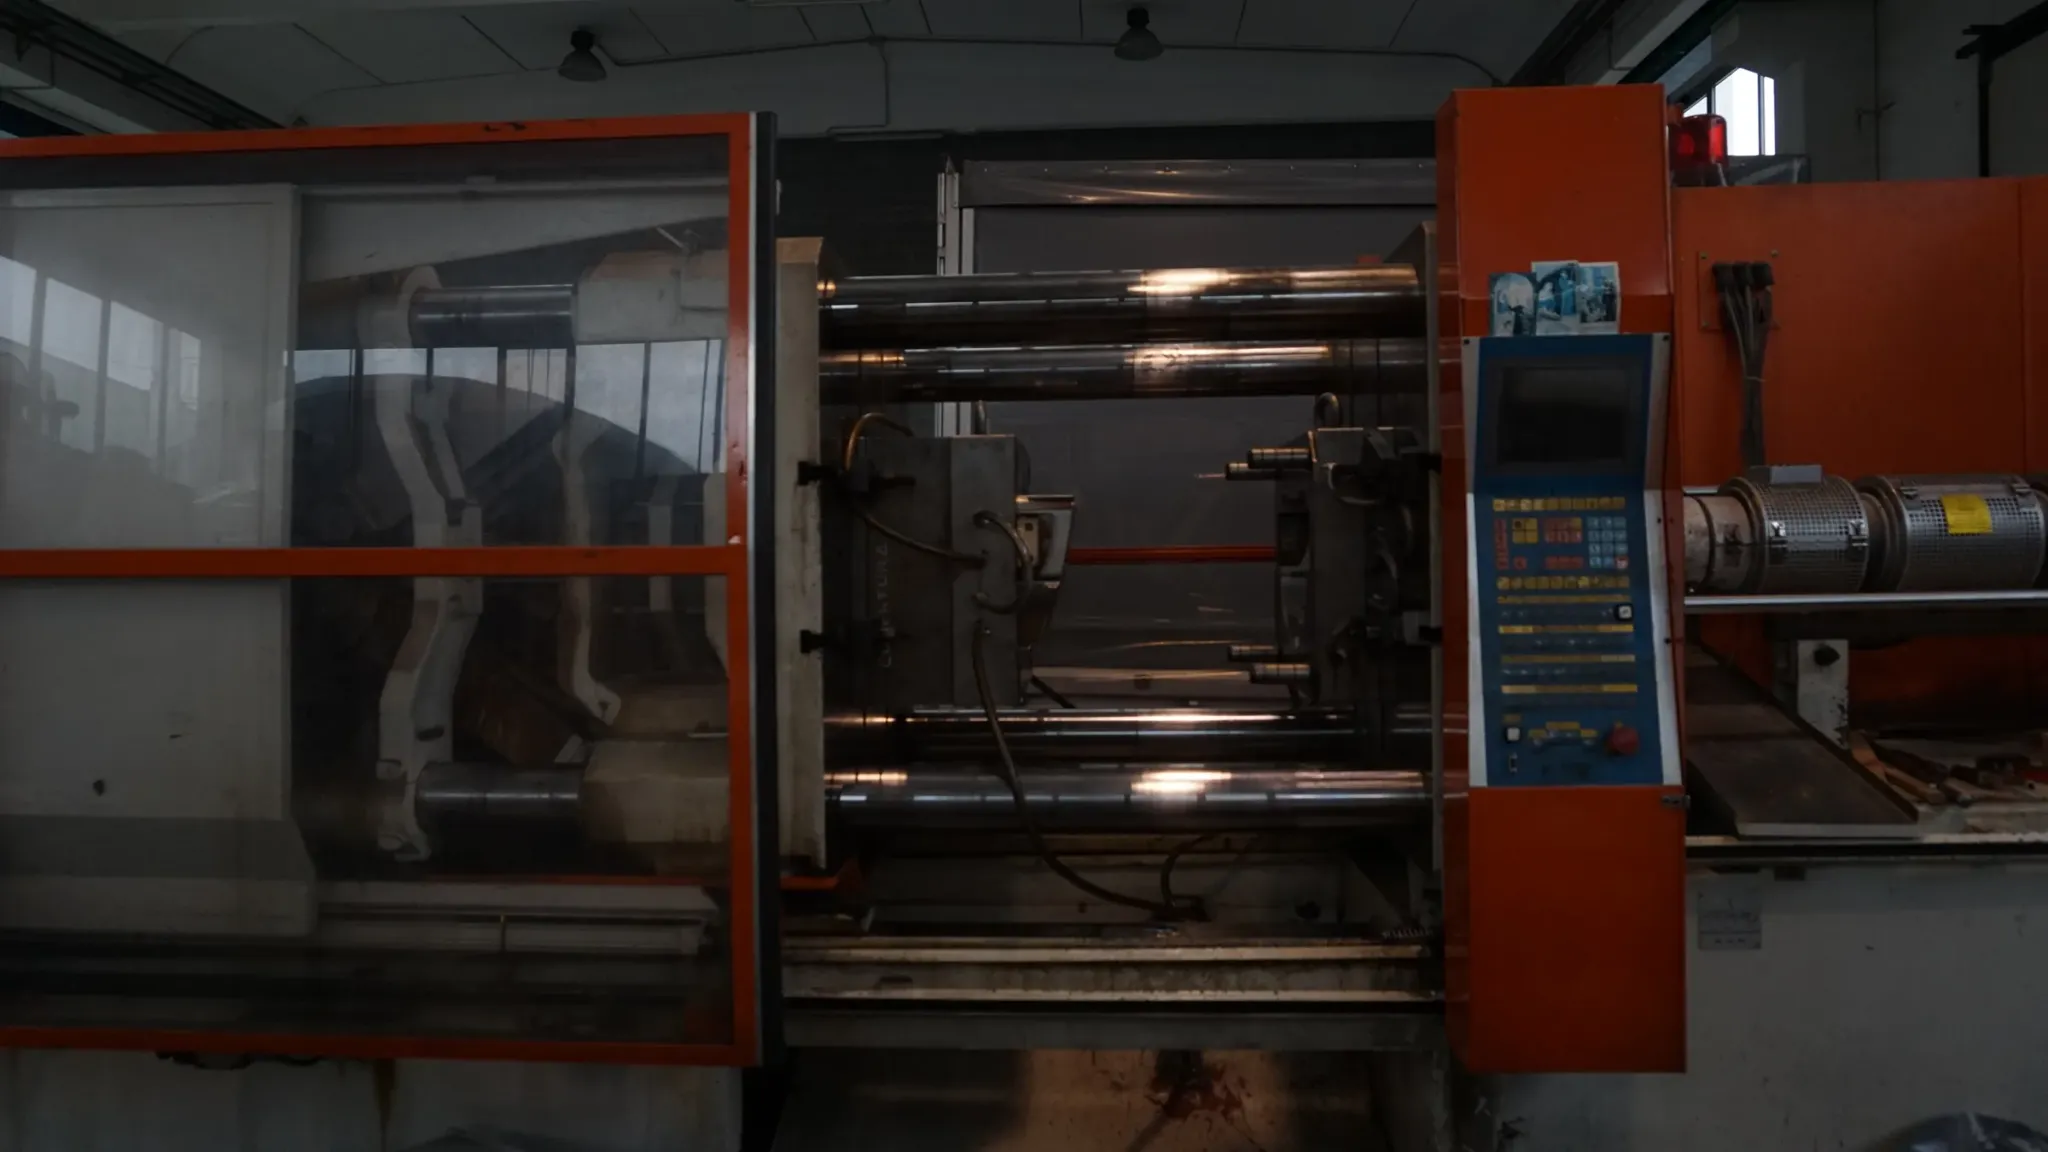
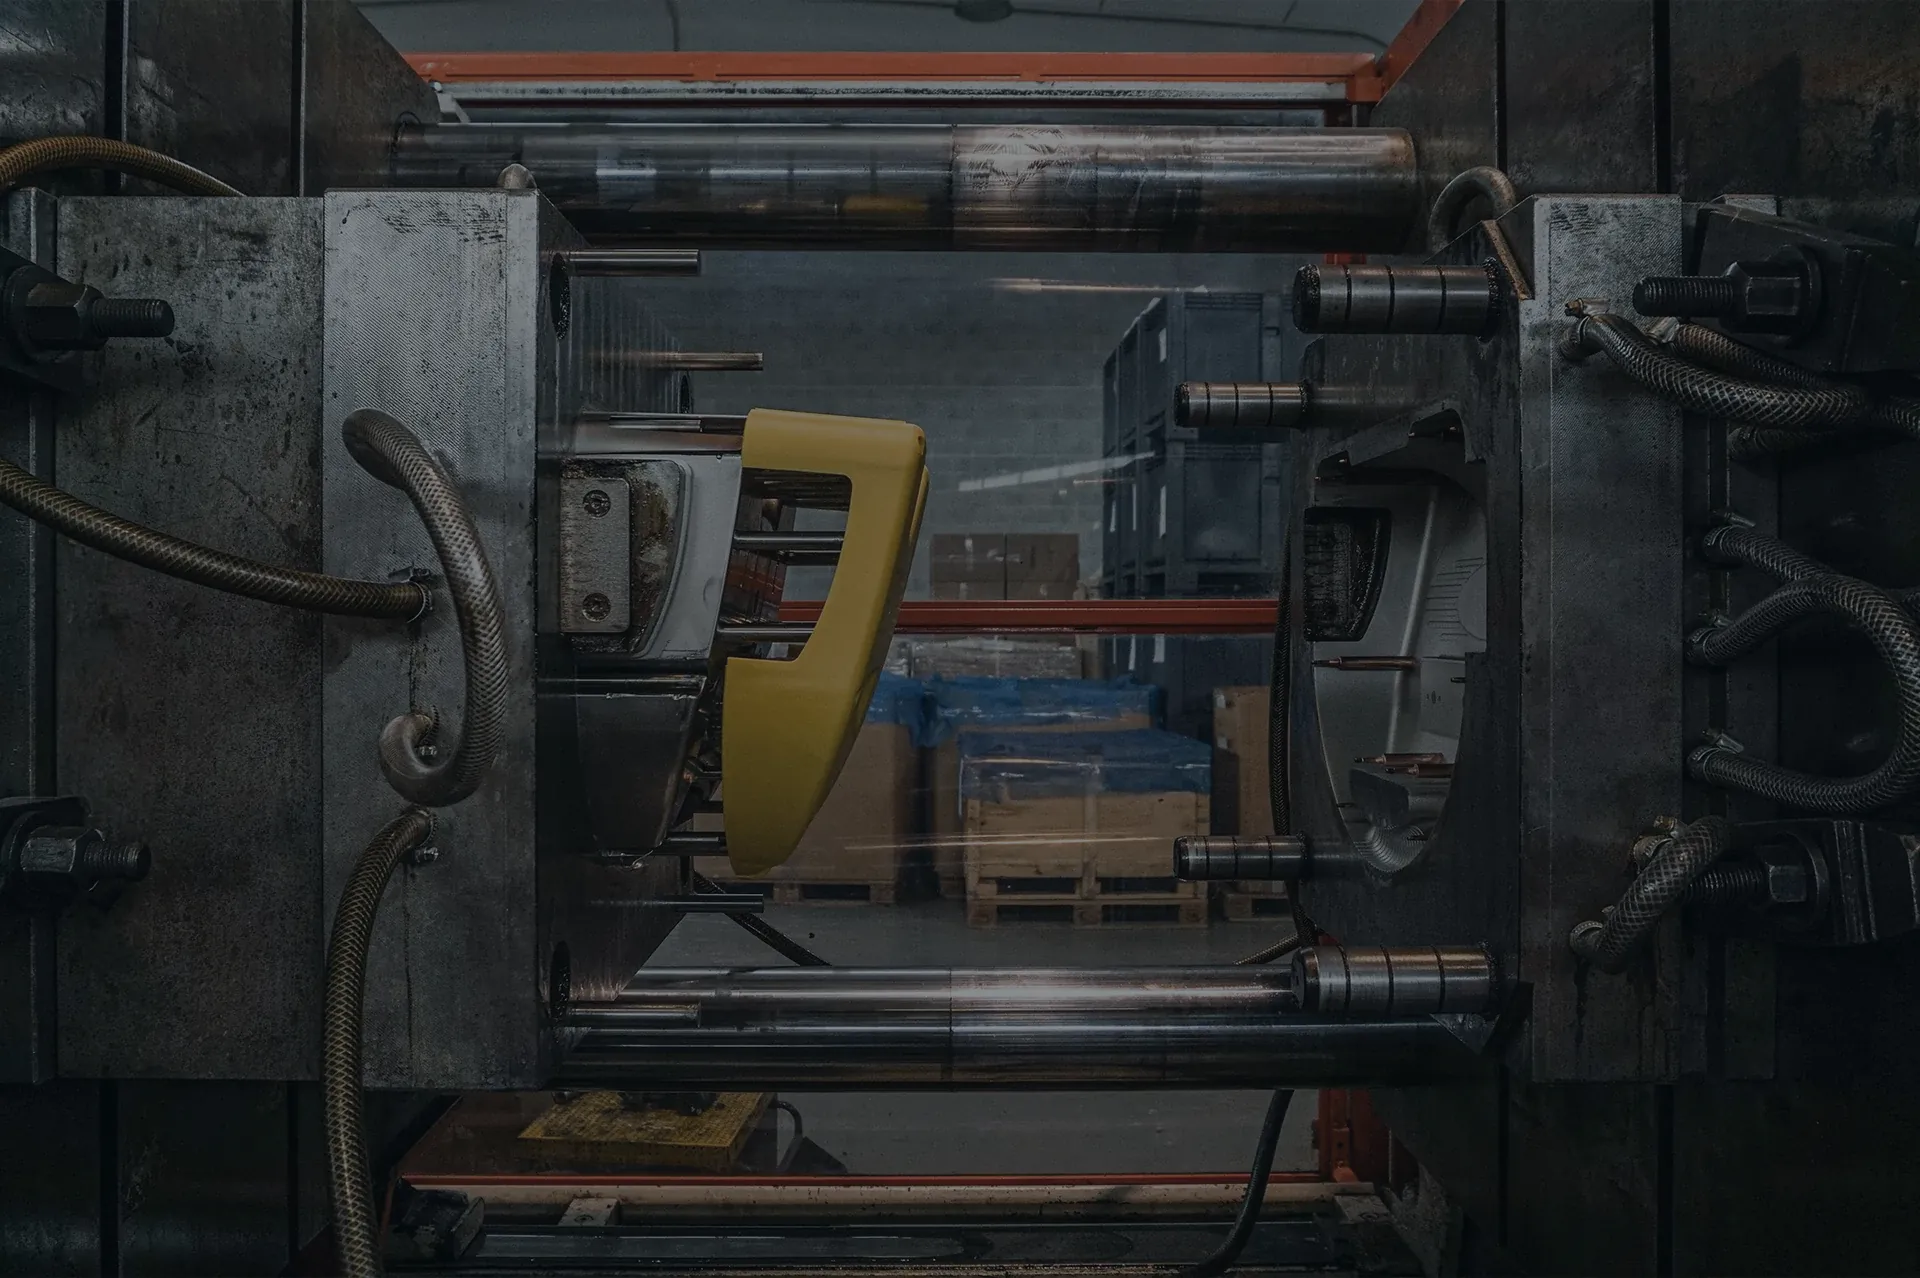
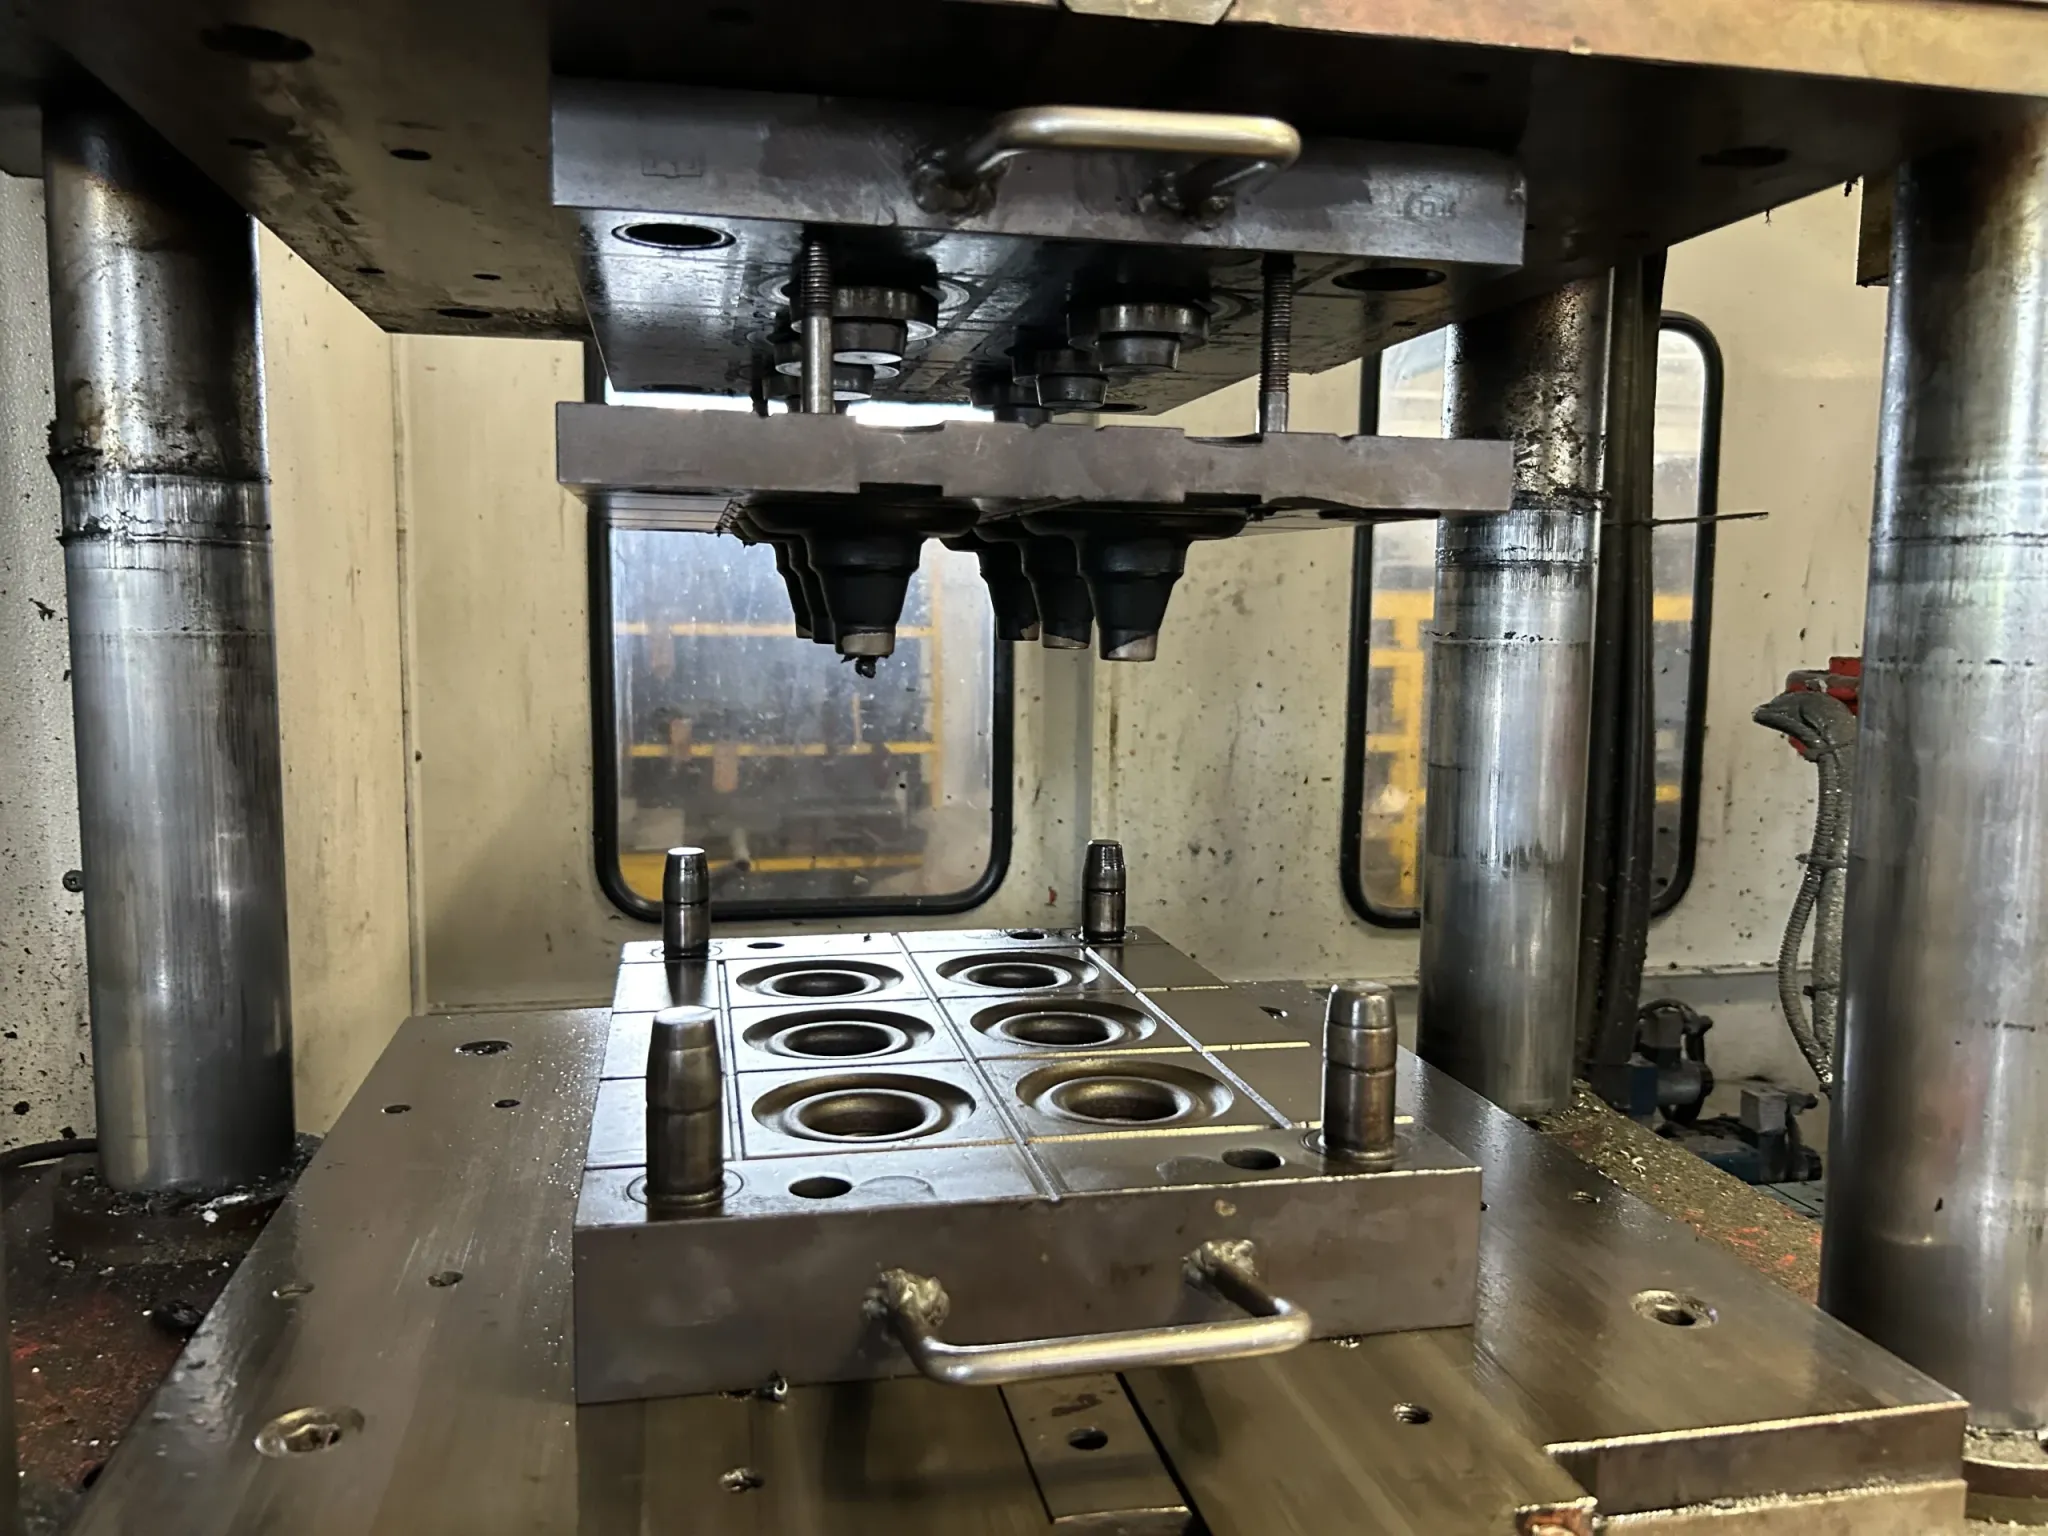
Injection moulding press at the Corti Srl plant
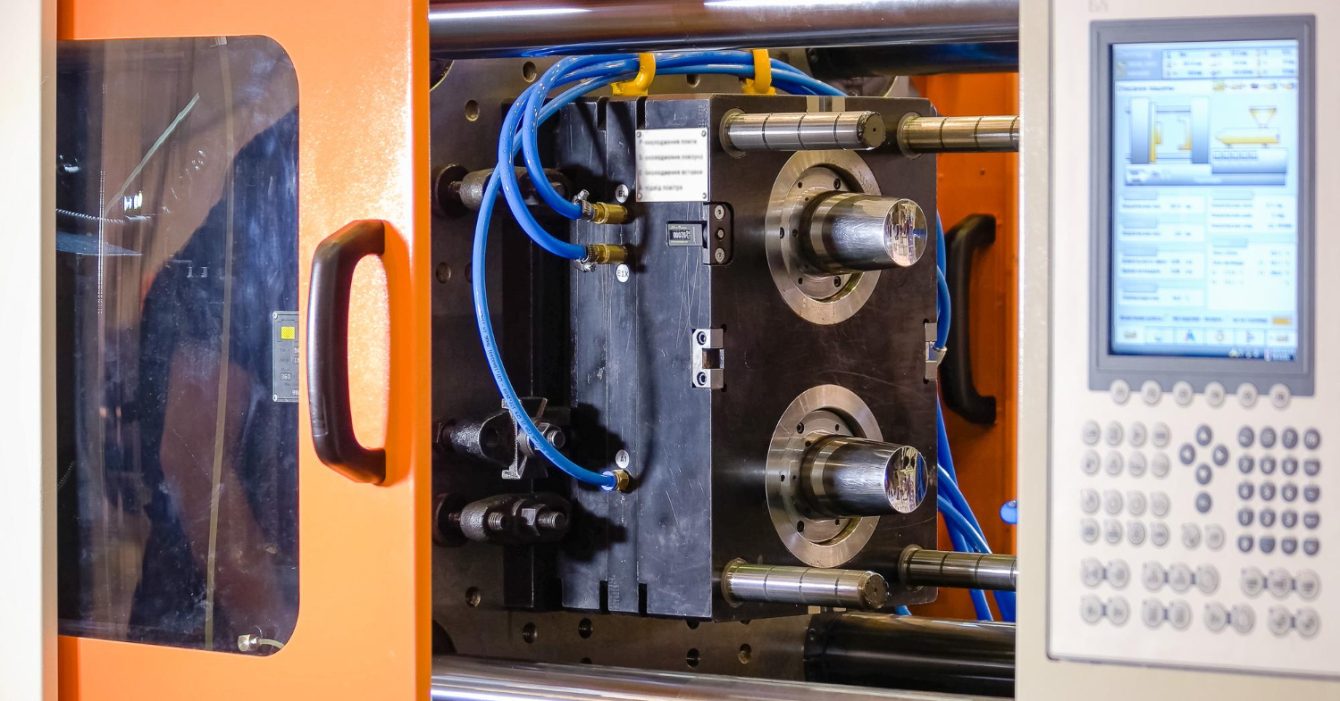
Mould mounted in an injection moulding press
Mould mounted in the press
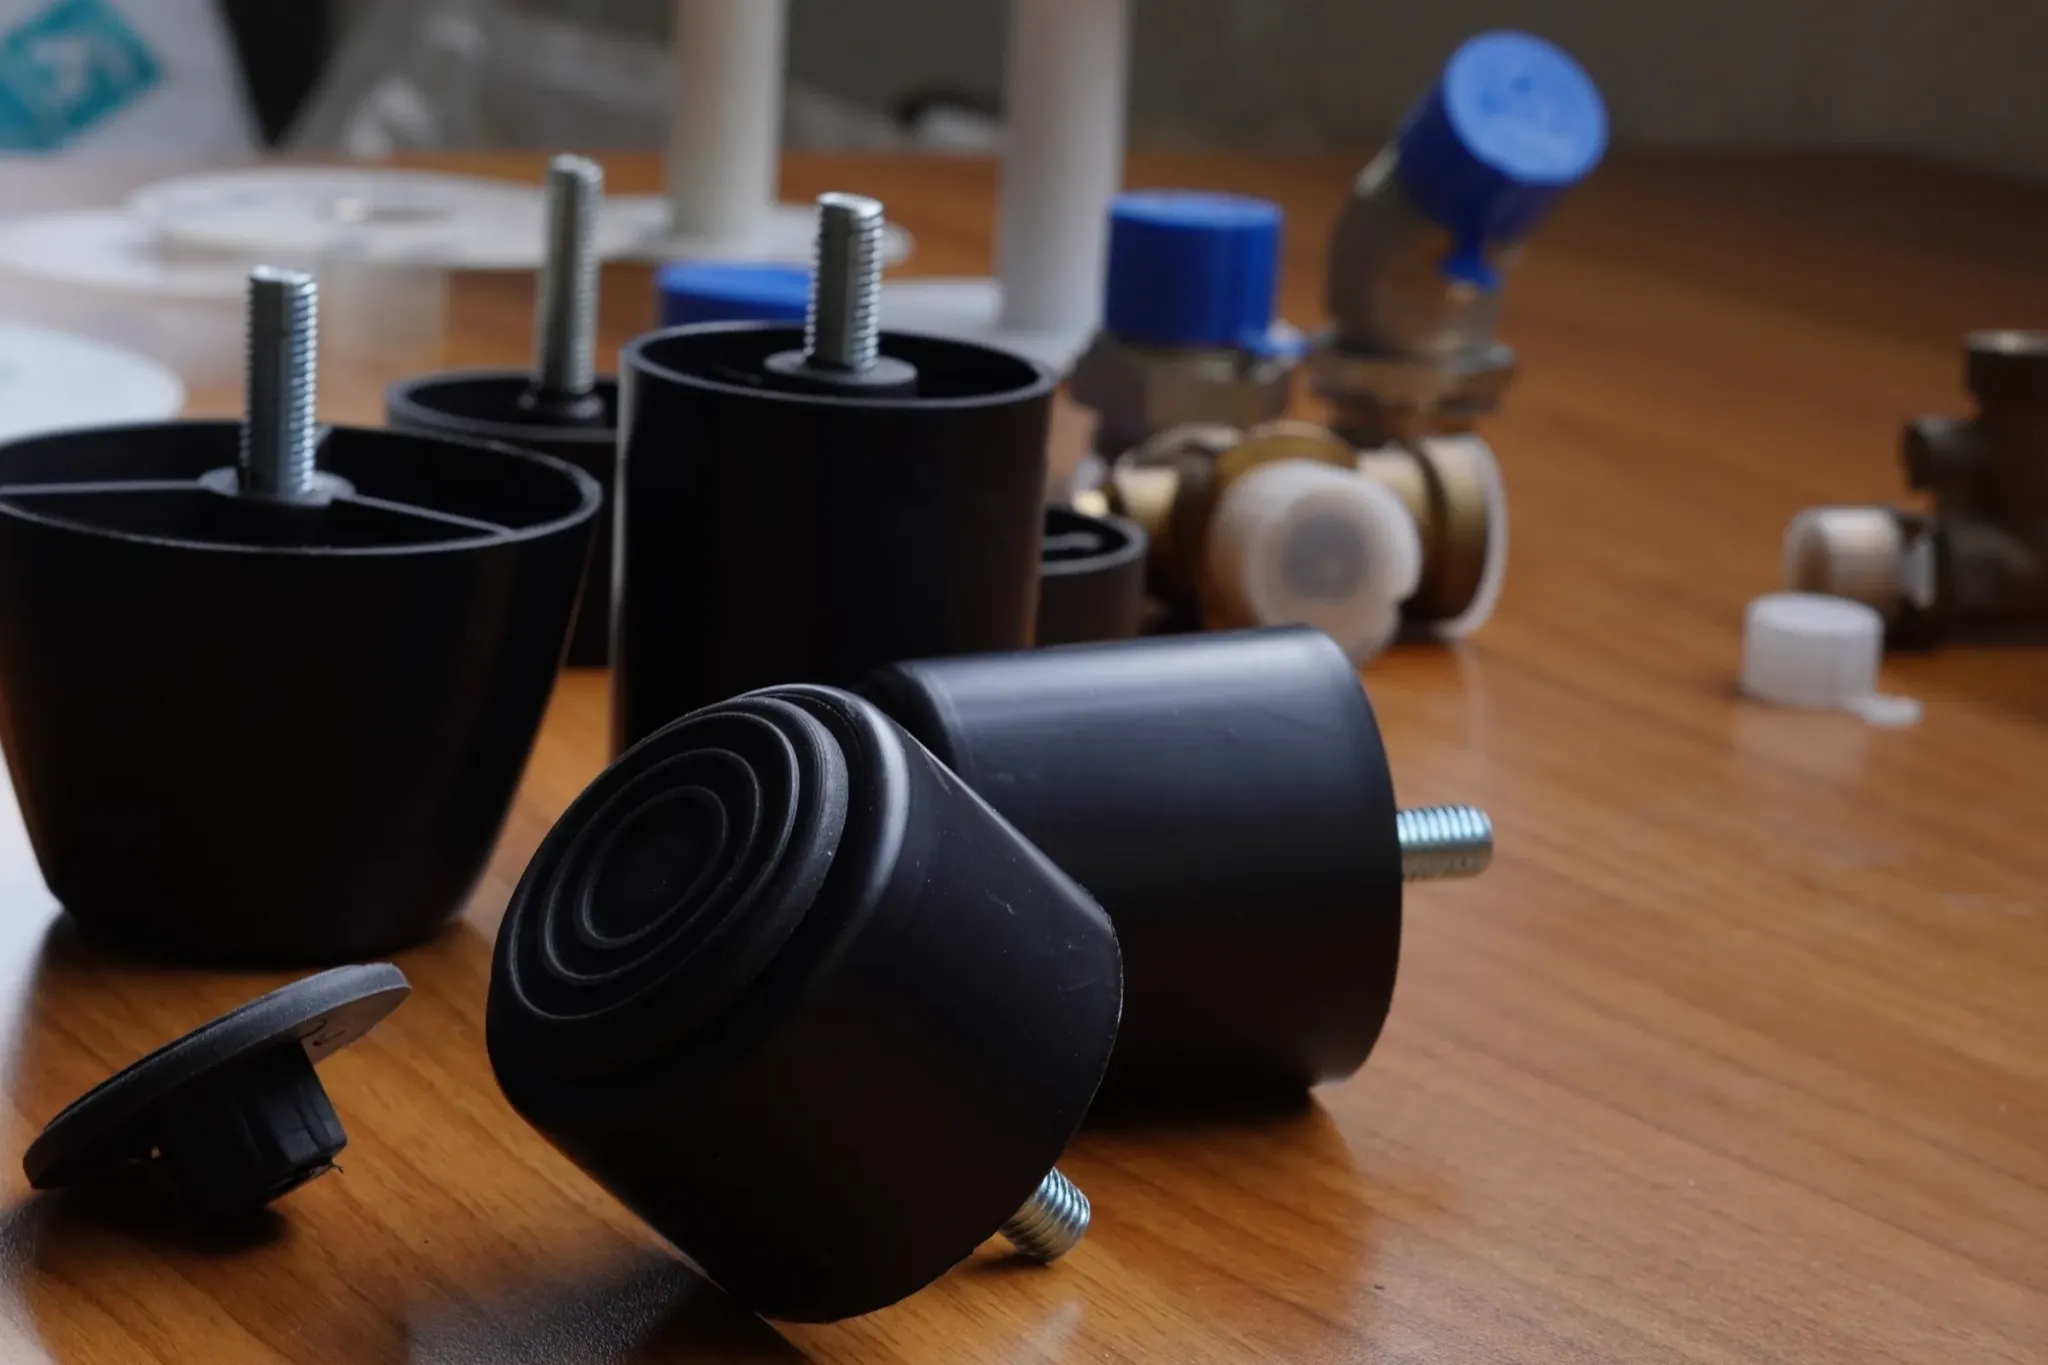
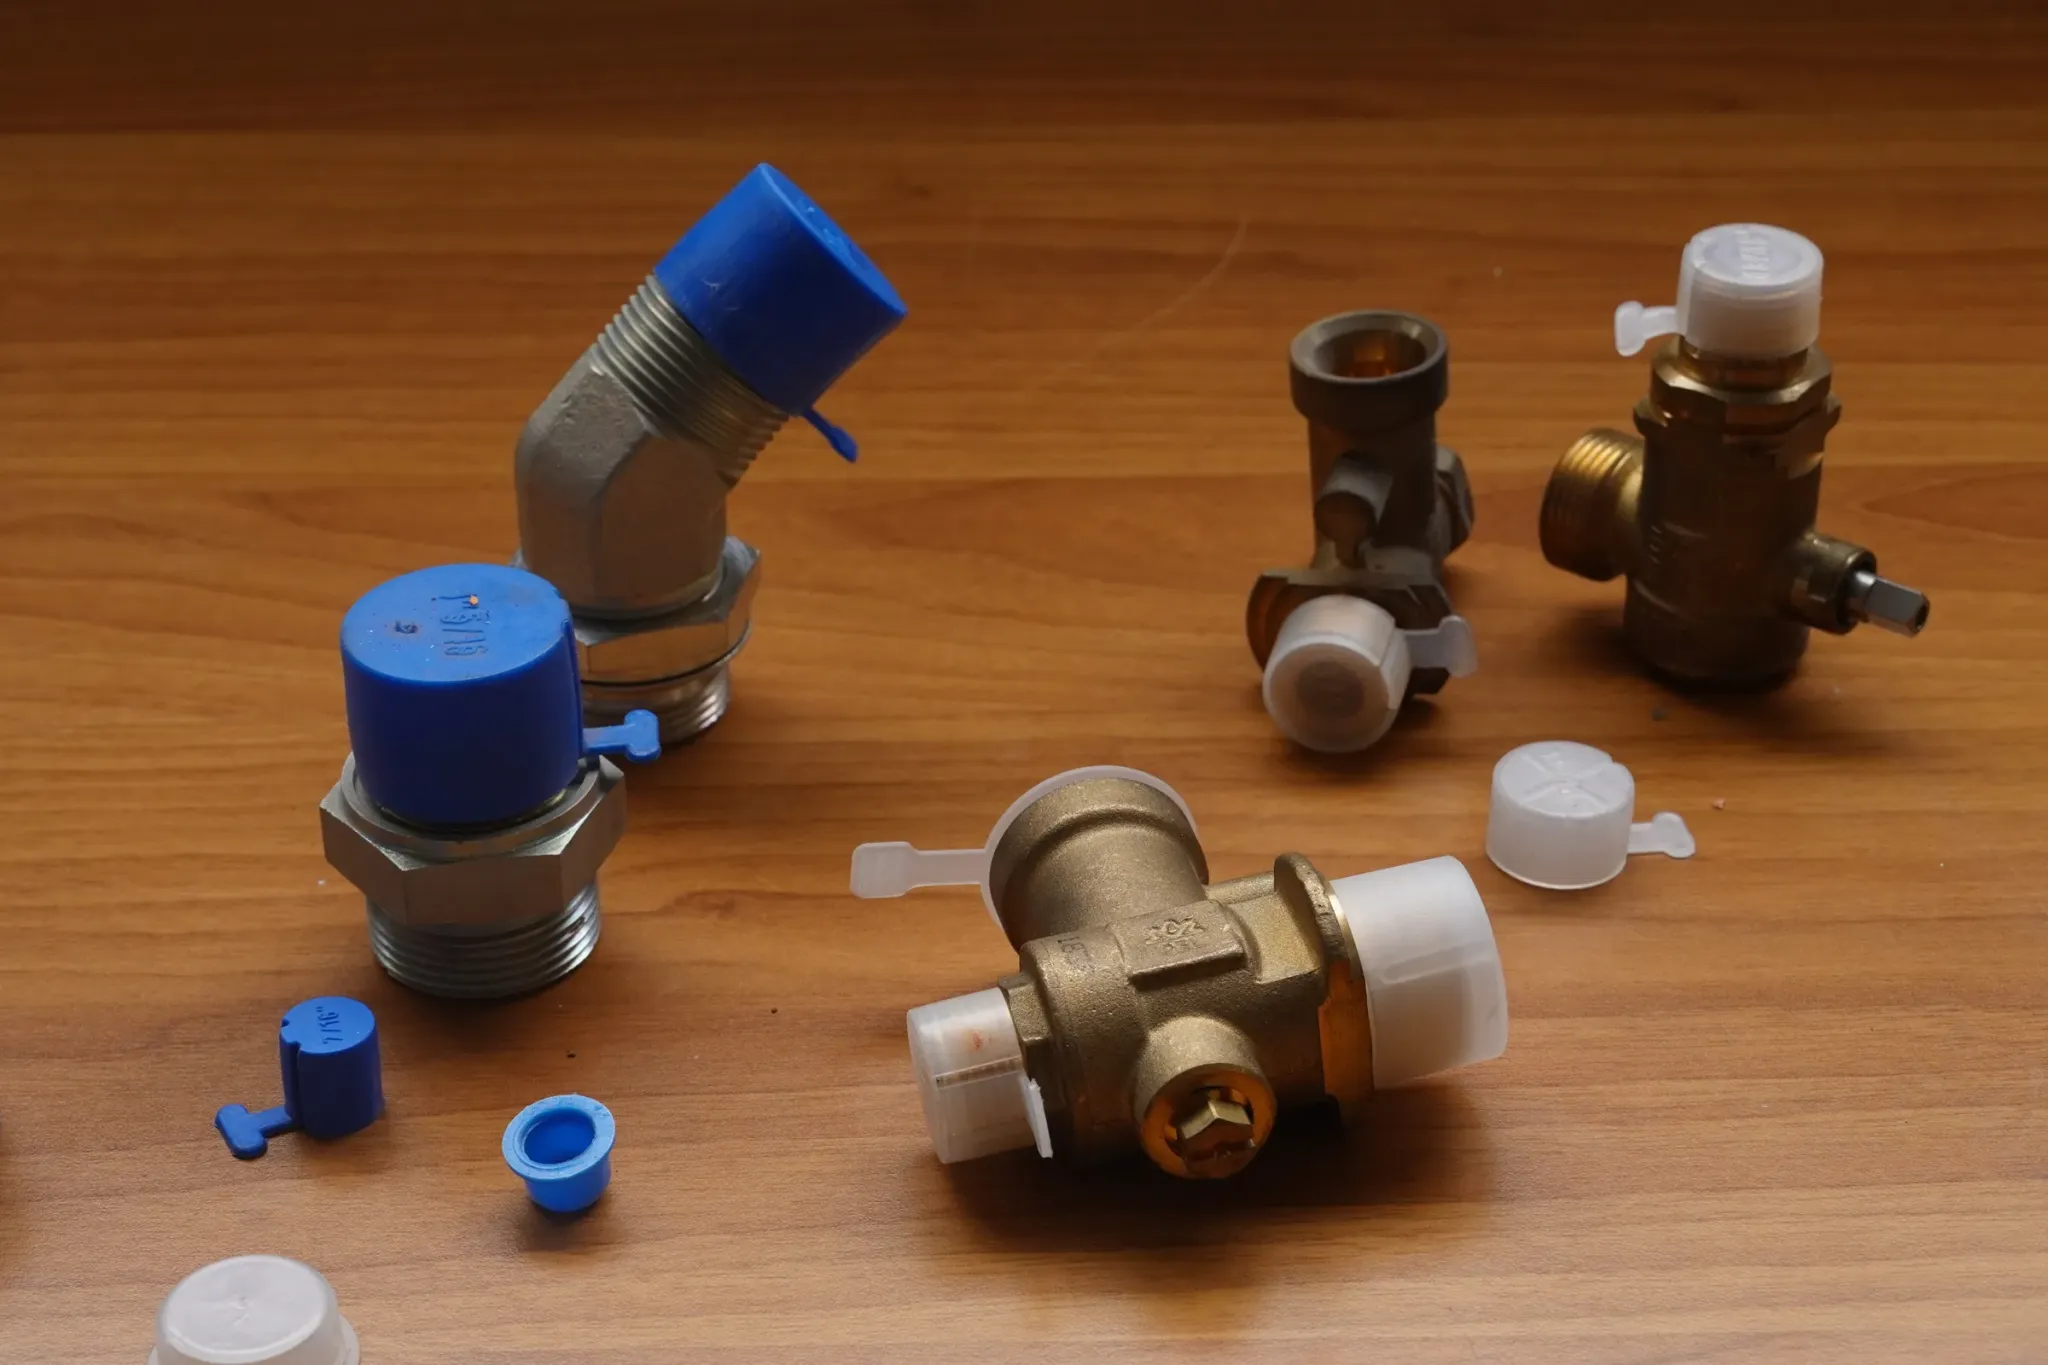
Injection-moulded plastic parts
Feet for tables and armchairs
Protective caps for hydraulic fittings

Read the full article

Rubber compression moulding

The rubber compound is compressed in a heated mould and vulcanised. Vulcanisation turns raw rubber into a cross-linked elastomer that is elastic, strong and durable.

Process stages

  1. Compound preparation The compound is chosen according to the conditions of use of the component (temperature, chemicals, stresses, hardness), then cut and weighed according to the cavity volume.
  2. Loading the mould As the mould closes, the compound is compressed until it fills the cavity. Any metal inserts are positioned beforehand.
  3. Vulcanisation It takes place at between 140 °C and 170 °C, for 10–90 minutes, depending on the compound and the size of the part.
  4. Removal from the mould Cooling and deflashing follow.

Why control matters

Temperature, pressure and time determine the quality of the part. Insufficient vulcanisation leaves the rubber too soft; excessive vulcanisation makes it stiff and brittle.

Open six-cavity compression mould in the press
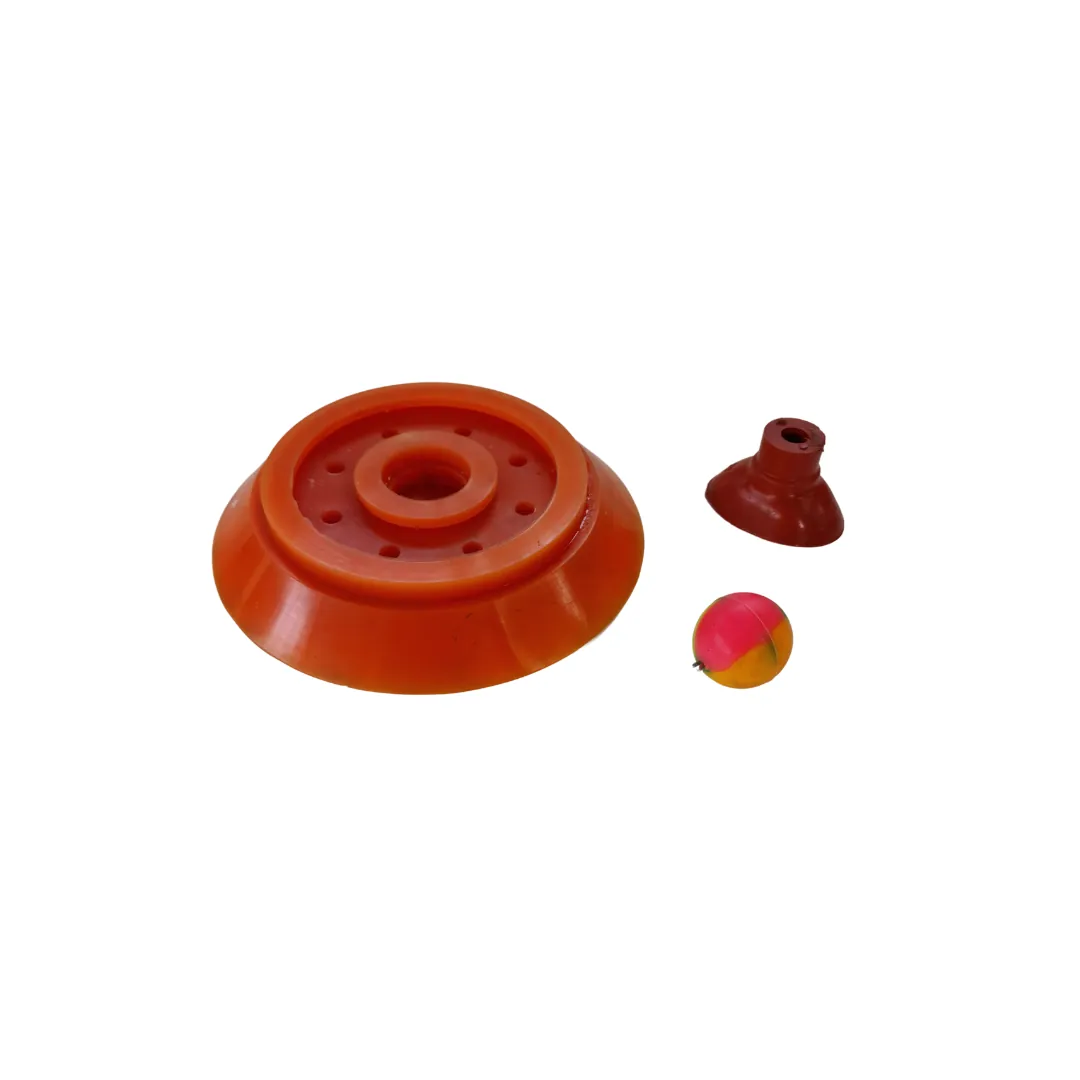
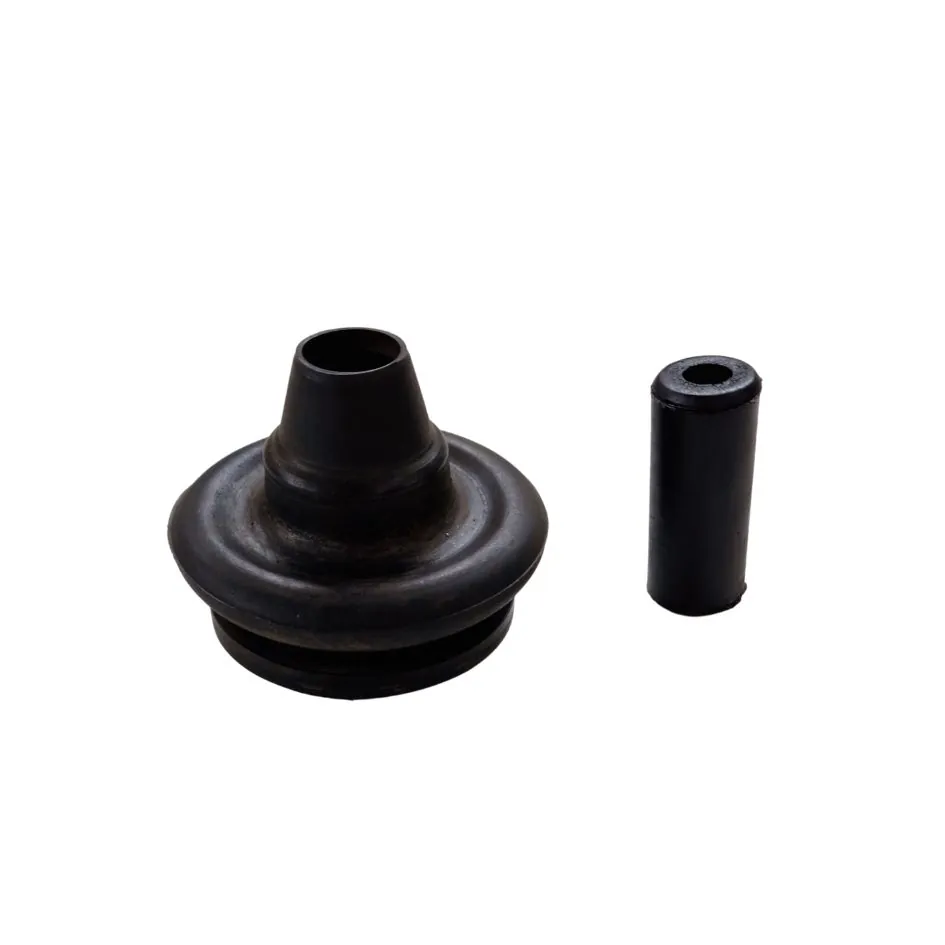
Compression-moulded rubber parts
Silicone parts
Silicone parts
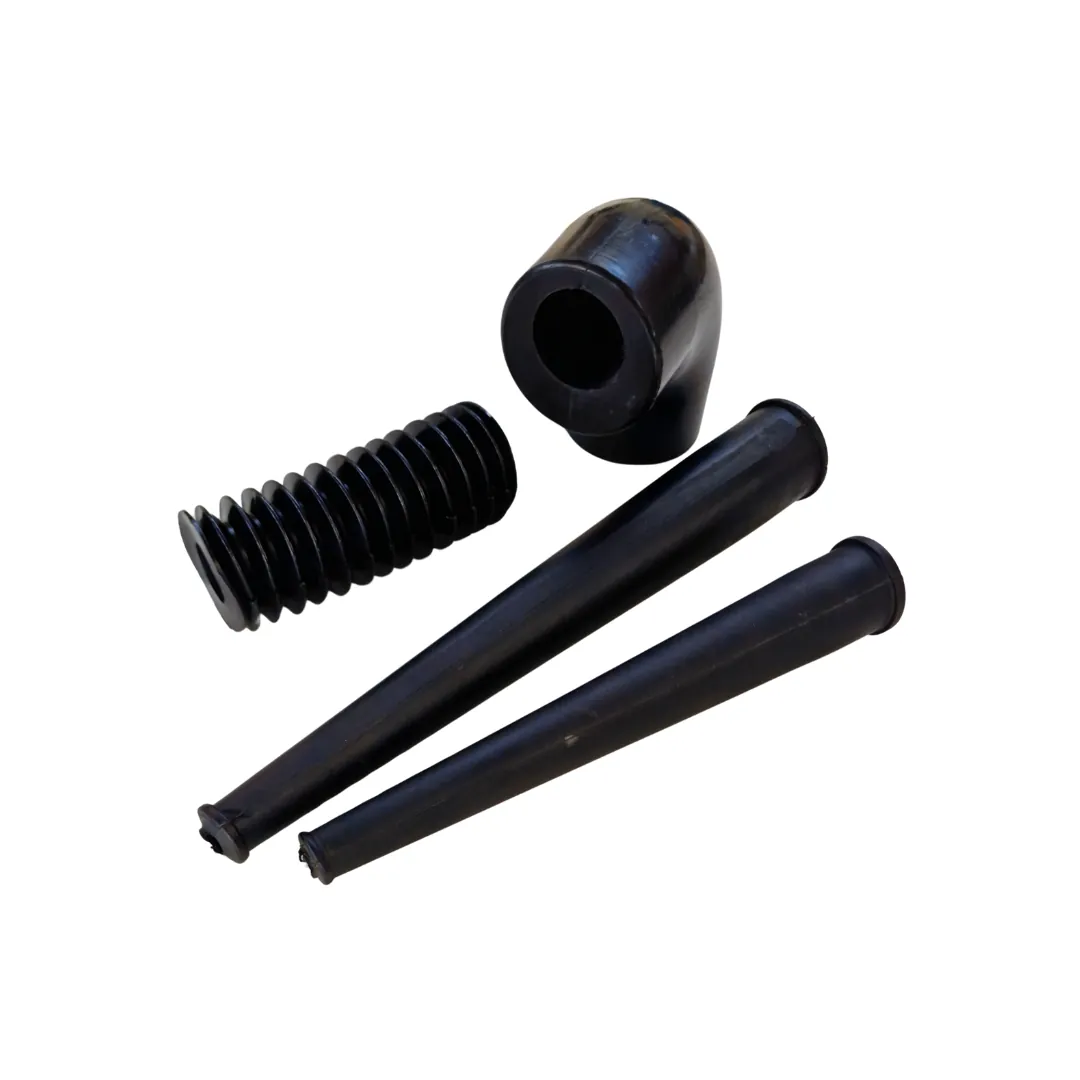
Bellows and components for the automotive sector

Read the full article

Rubber-to-metal overmoulding

A metal insert is permanently bonded to rubber directly in the mould. The result is a pre-assembled composite part: the metal provides rigidity, the rubber elasticity, sealing and vibration damping.

Process stages

  1. Insert preparation The insert is cleaned and shot-blasted, then treated with a specific primer chosen according to the metal and the elastomer.
  2. Rubber preparation The rubber is weighed and cut into strips.
  3. Moulding and vulcanisation The insert is placed in the mould and the rubber is compressed around it; vulcanisation takes place at between 140 °C and 170 °C, for 10–90 minutes.
  4. Removal from the mould and deflashing

Double bond

The bond is both chemical (primer and cross-linking) and mechanical (undercuts designed into the insert).

Which process

Thermoset elastomers (EPDM, NBR, silicone) are overmoulded by compression; thermoplastic elastomers (TPE, TPU, SEBS) by injection.

Advantages

  • permanent structural adhesion
  • no gluing or manual assembly
  • two materials with different functions in one part
  • complex geometries
  • longer service life
  • lighter components

Applications by sector

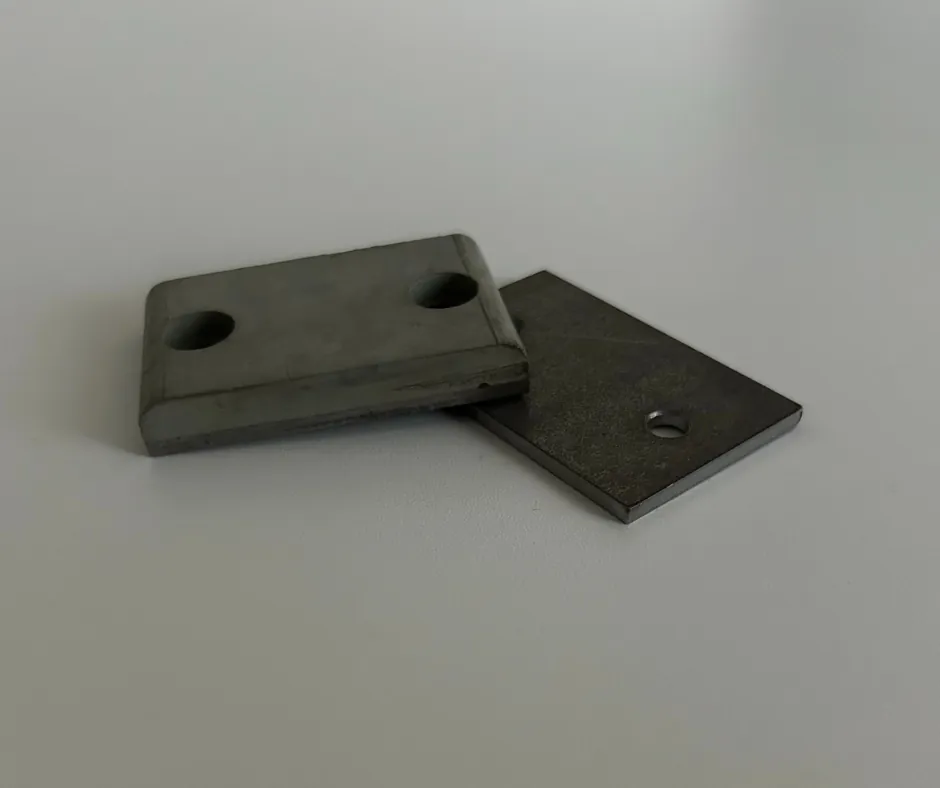
Rubber cleat for conveyor belt
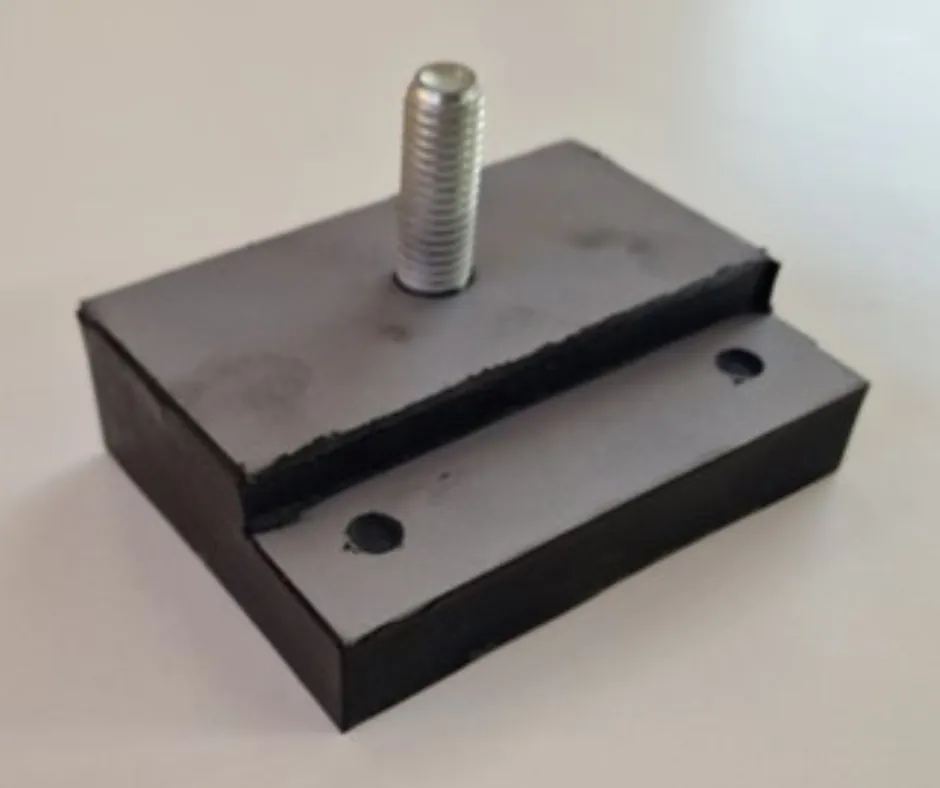
Rubber-to-metal anti-vibration buffer
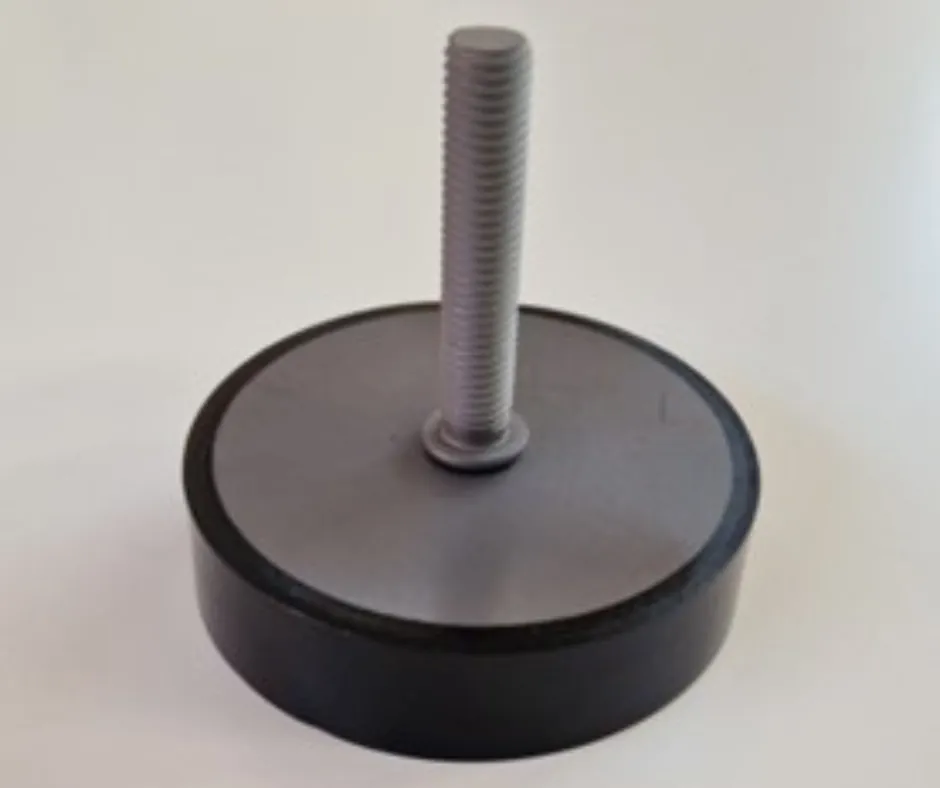
Rubber-to-metal anti-vibration mount
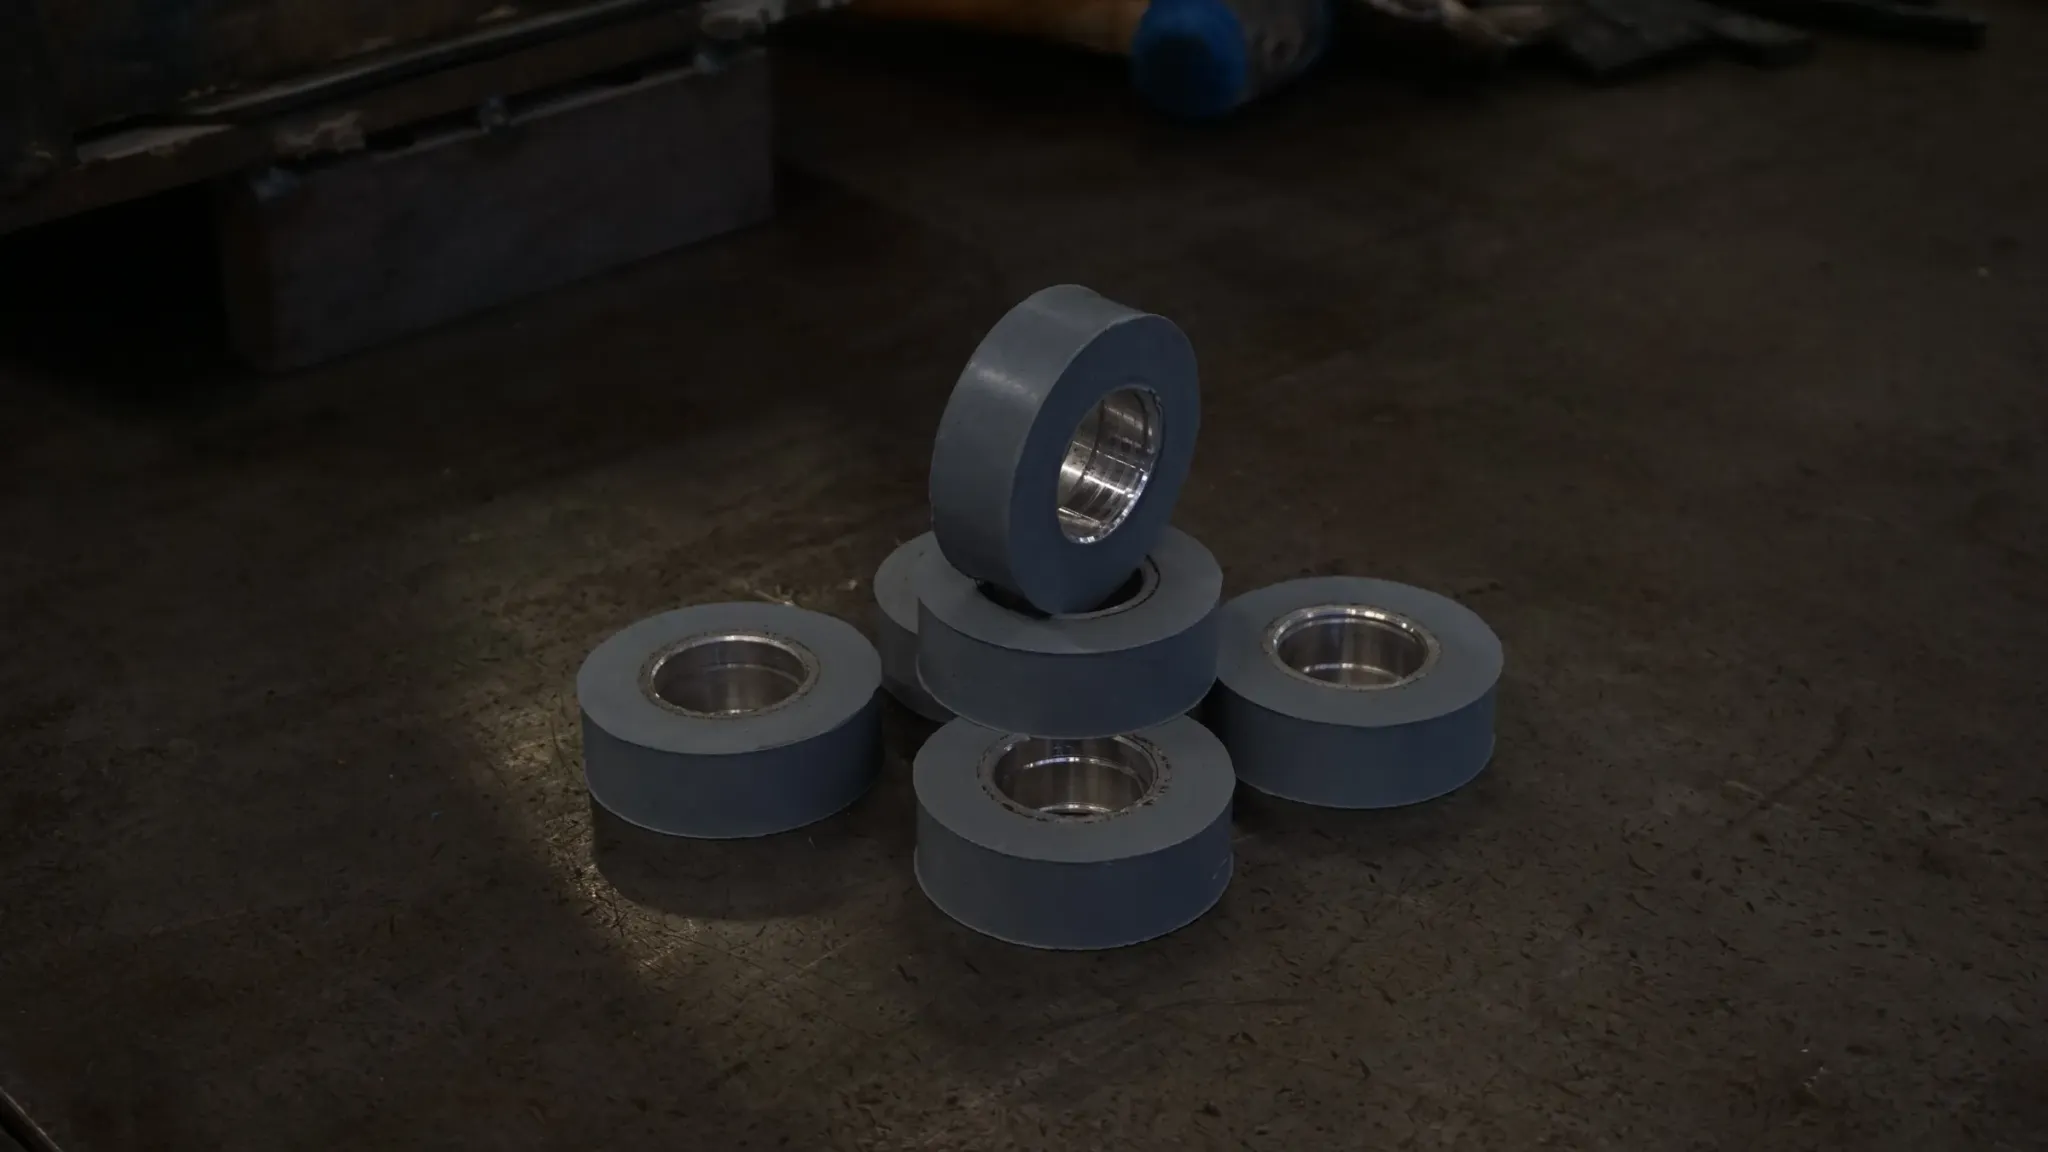
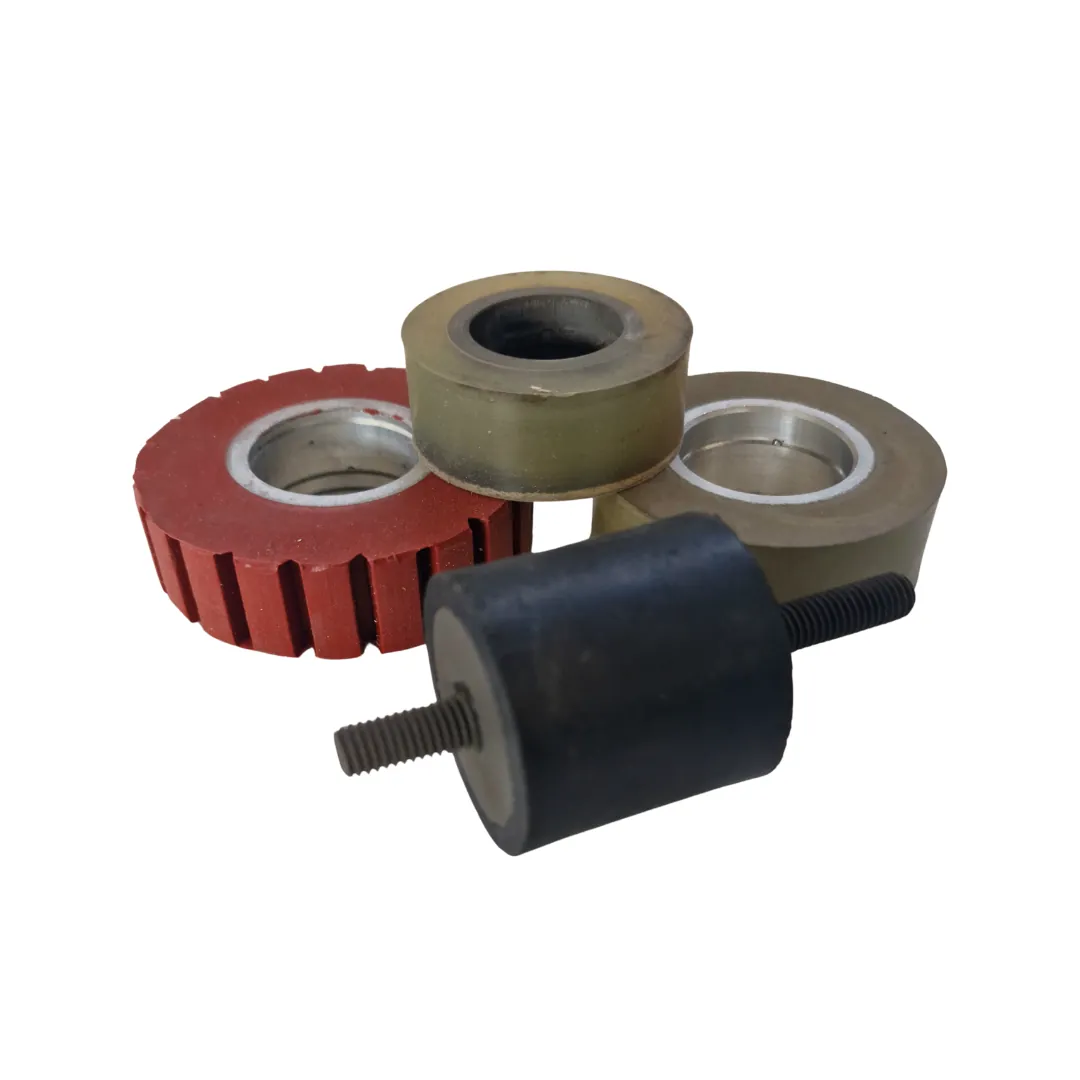
Wheels with rubber-to-metal bonding

Read the full article

Parts and details

Some of the parts produced by Corti Srl, grouped by family.

Sustainability in our production processes

The practical side of sustainability in our plant.

  1. New-generation, low-energy press fleet (Industry 4.0).

  2. Real-time monitoring of moulding parameters, which reduces scrap.

  3. Thermoplastic scrap is reground and fed back into production, where the material allows.

  4. Vulcanised rubber cannot be remelted, but offcuts and end-of-life components can be recovered with dedicated technologies.

  5. Reuse of intact pallets, including those received from suppliers.

  6. Separate collection of production waste.

Sustainable materials and PFAS alternatives

Sectors

Sectors we serve

We design moulds and manufacture made-to-drawing components for companies in every industrial sector. These are the main ones we work in.